


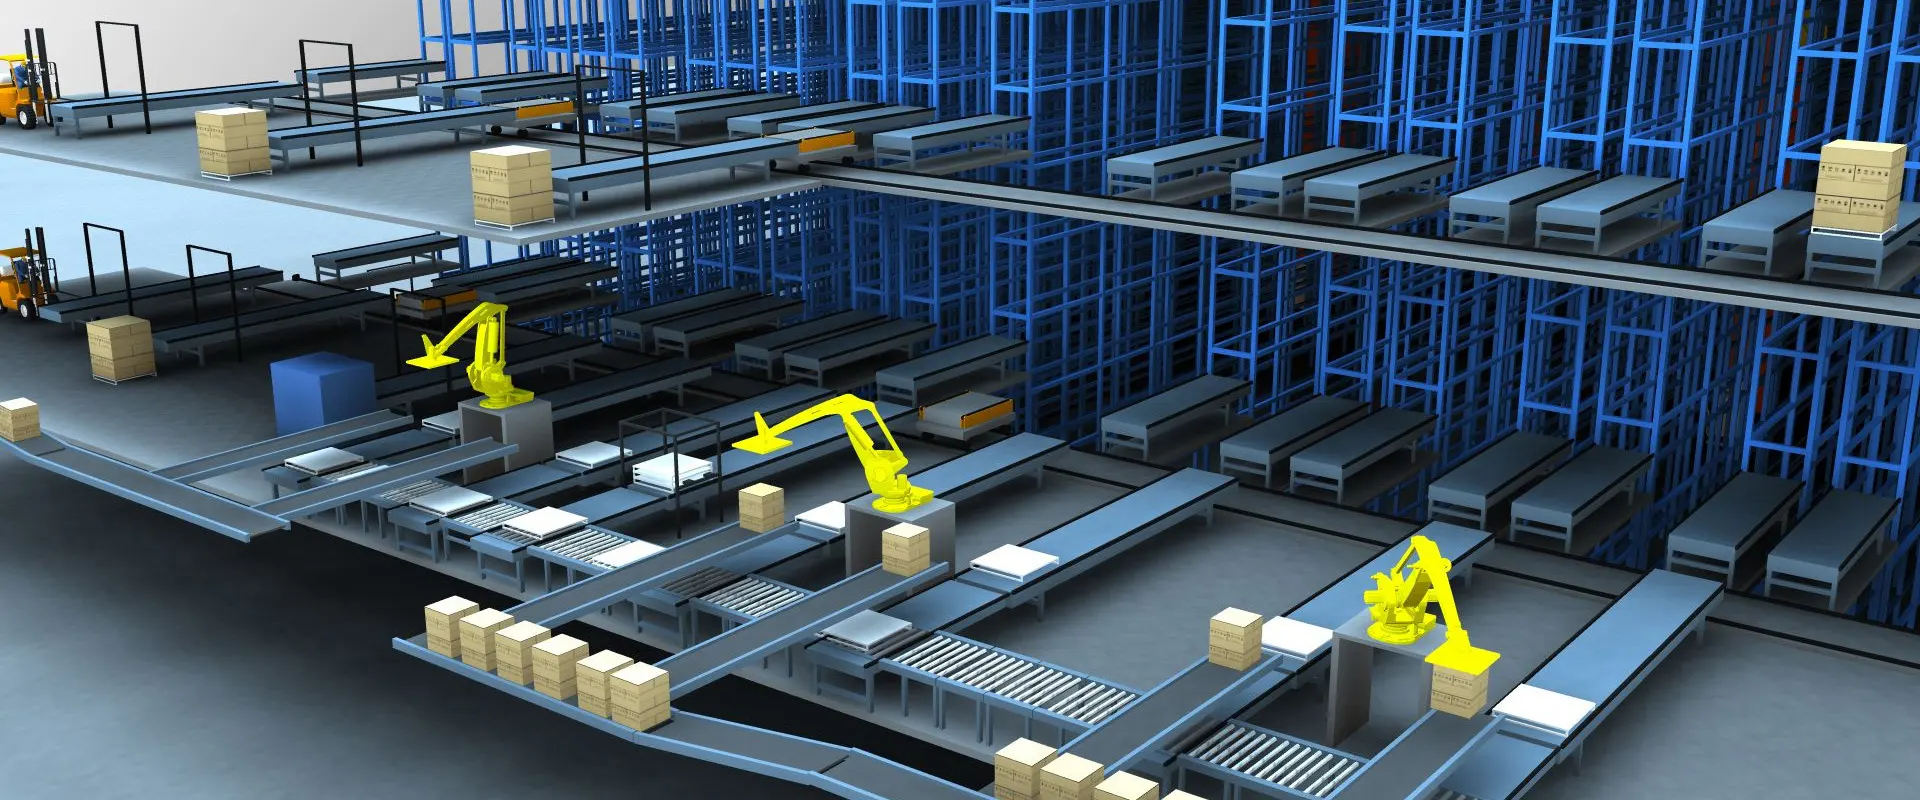
High-Capacity Sorting Conveyors Support the Rapid Growth of Modern Logistics
May 07,2026

As global e-commerce and express delivery industries continue to expand, logistics companies are facing increasing pressure to process larger parcel volumes with greater speed and precision. High-capacity sorting conveyors have become a critical solution for meeting these operational challenges, enabling automated and efficient parcel handling in modern distribution centers.

High-capacity sorting conveyors are designed to transport and sort massive volumes of parcels continuously and accurately. Equipped with advanced scanning technology, sensors, and intelligent control systems, these conveyors automatically identify and route items to their designated destinations. By integrating high-speed sorting mechanisms with stable conveying performance, the system ensures smooth material flow even during peak operating periods.
One of the most significant advantages of high-capacity sorting conveyors is their exceptional throughput capability. These systems can process thousands or even tens of thousands of parcels per hour, making them ideal for large-scale e-commerce warehouses, courier hubs, and airport logistics centers. During major shopping festivals or seasonal peaks, high-capacity sorting conveyors help businesses maintain stable operations and avoid bottlenecks.
Accuracy is another essential feature. Automated scanning and sorting technologies reduce the risk of human error, ensuring that parcels are delivered to the correct destinations quickly and efficiently. Improved sorting precision also helps minimize operational costs associated with returns, delays, and misrouted shipments.
Flexibility and scalability are key strengths of modern high-capacity sorting conveyors. The systems can handle parcels of different sizes, weights, and packaging types, ranging from small envelopes to bulky cartons. Modular configurations allow businesses to expand sorting capacity or adapt system layouts as operational demands evolve. Integration with warehouse management systems (WMS) further improves visibility and real-time monitoring capabilities.
In addition to operational efficiency, high-capacity sorting conveyors contribute to safer working environments. By automating repetitive and physically demanding sorting tasks, these systems reduce labor intensity and lower the risk of workplace injuries. Employees can instead focus on supervision, quality control, and higher-value logistics activities.
Modern high-capacity sorting conveyors are also equipped with intelligent diagnostics and predictive maintenance technologies. These features help identify potential equipment issues before failures occur, reducing downtime and ensuring long-term operational reliability.
In conclusion, high-capacity sorting conveyors are playing an increasingly important role in modern logistics infrastructure. Their combination of speed, precision, scalability, and automation enables logistics providers to handle rapidly growing parcel volumes efficiently while maintaining high service standards in a highly competitive market.
PREVIOUS:


-
Our mission is to be recognised as class leading solution providers for materials handling and automation systems across all industry sectors.